Best Gray Iron Casting Practices for Superior Strength and Durability
2026-10-01
Gray iron gets a bad rap when someone skips the fundamentals—pouring too hot, ignoring inoculation, or letting section thickness dictate weakness. At Zhaoyuqi, we've seen how small, deliberate choices in gating, risering, and alloying can push tensile strength and fatigue life far beyond textbook expectations. This isn't another generic list of do's and don'ts. We're sharing the exact practices we rely on to produce gray iron castings that survive shock loads, thermal cycling, and decades of service. Read on if you want castings that outperform the spec sheet, not just meet it.
Melt Chemistry Adjustments That Outperform Standard Specifications
Conventional melt chemistry controls leave gaps that only become visible after weeks of production. By shifting from fixed checklists to real-time slag-metal equilibrium tracking, operators can anticipate where standard specs underperform and push the heat into a more stable operating window. This means measuring the oxidation potential not just at tap, but at multiple points during refining, and adjusting deoxidizer additions based on actual oxygen activity rather than nominal weight. The result is a heat that meets the certificate with room to spare, reducing the need for re-blows or late furnace corrections.
Another overlooked lever is the deliberate use of residual elements to shift inclusion morphology. Instead of simply hitting maximum allowable sulfur or phosphorus, a tuned magnesium-to-calcium ratio can turn otherwise harmful inclusions into finely dispersed globular oxides that improve downstream formability. This approach goes beyond standard specifications because it treats chemistry not as a set of upper and lower limits, but as a dynamic balance between refining kinetics, slag basicity, and bath temperature. In practice, a small increase in slag viscosity combined with a reduced aluminum aim can outperform a textbook-perfect analysis by cutting total oxygen late in the heat.
The biggest gains come from linking ladle metallurgy data back to final product performance. Rather than accepting a heat as “in spec” the moment it passes the spectrometer, operators can track the ratio of free oxygen to soluble aluminum throughout the ladle treatment and adjust argon stirring intensity or wire feed speed accordingly. This closed-loop feedback often requires no extra alloys, only better timing and sequencing. Heats refined this way routinely show tighter hardenability bands and fewer surface defects, even when the certified chemistry looks identical to a conventionally treated batch.
Pouring and Cooling Rates: Where Strength Is Actually Determined
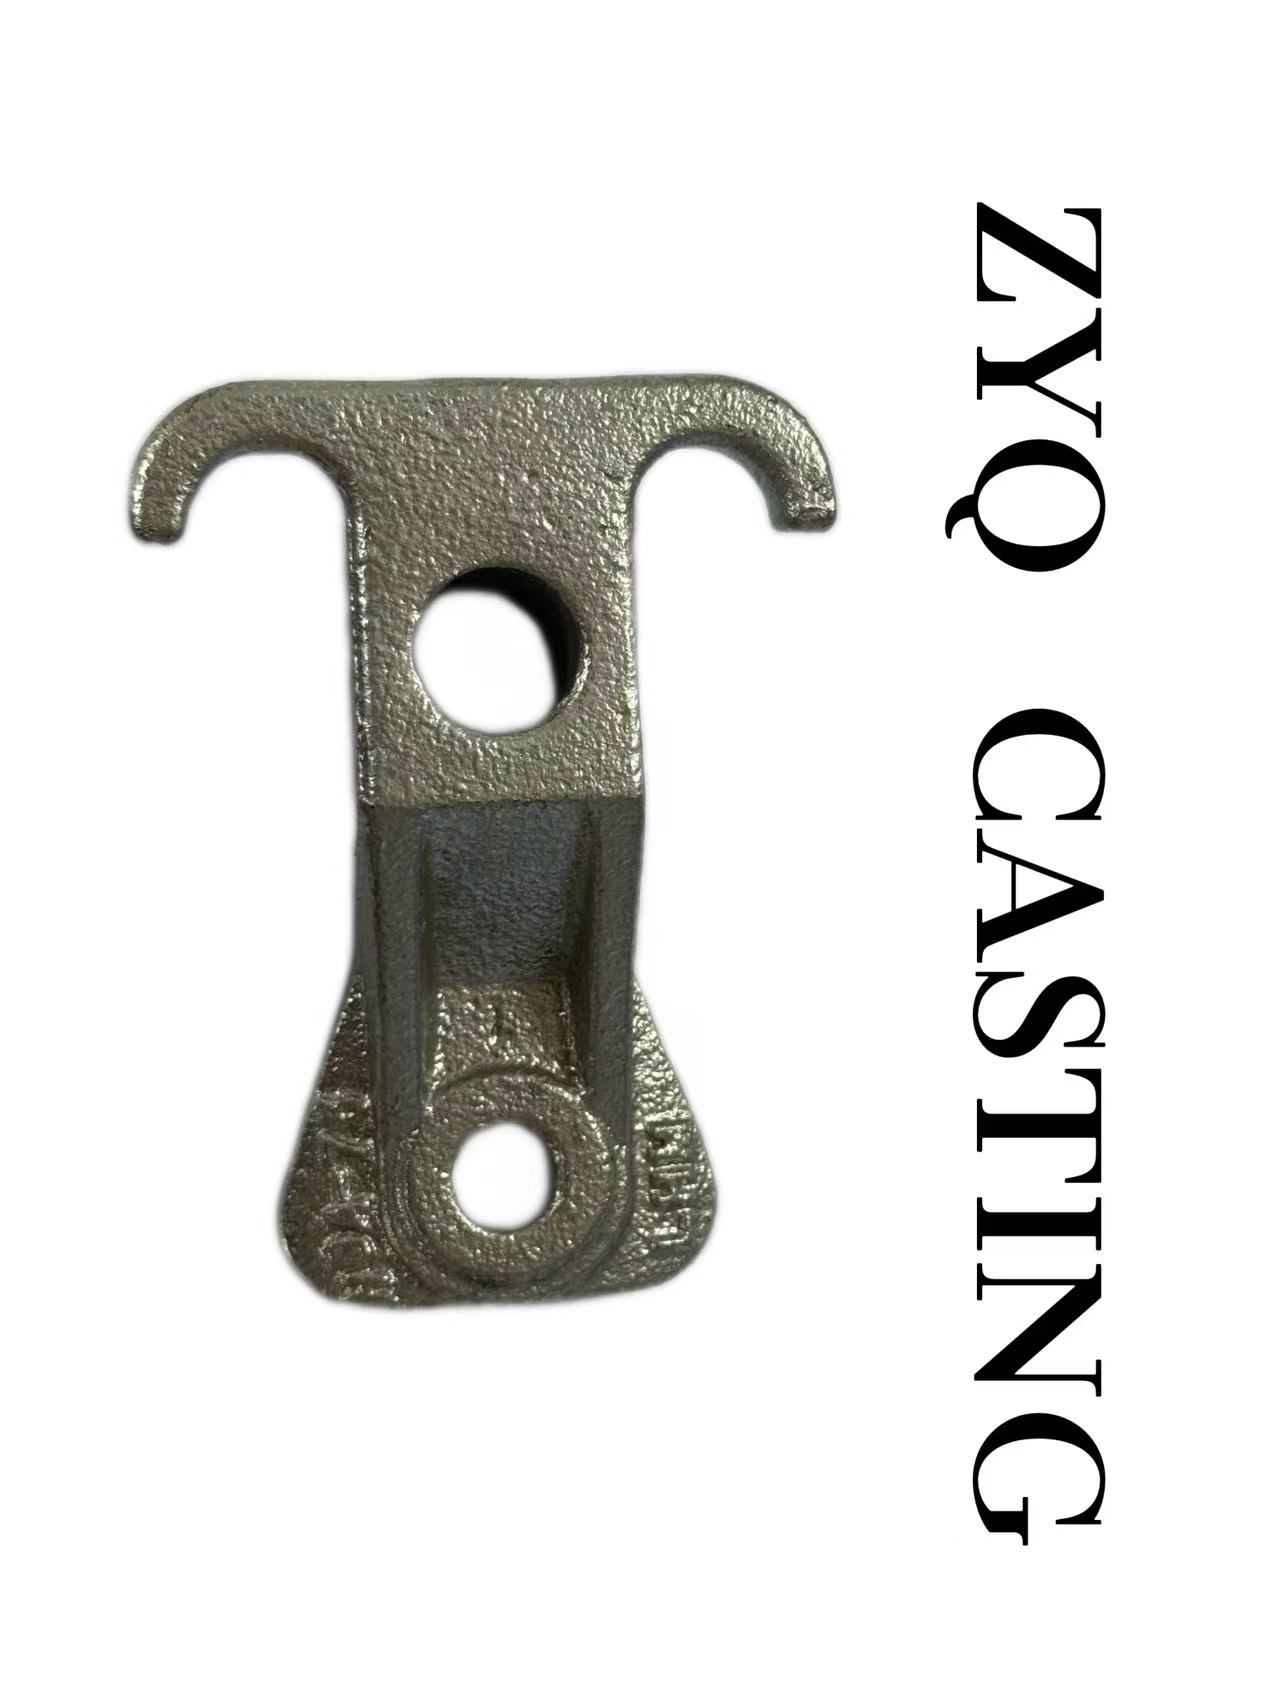
In most metalcasting discussions, people fixate on alloy chemistry or heat treatment, but the real battlefield for mechanical strength is how the liquid metal enters the mold and how quickly it leaves the liquid state. A slow, lazy pour can introduce oxides and air pockets that become internal notches, quietly subtracting from tensile strength long before any testing. Pushing the metal too fast, on the other hand, creates turbulence, erodes sand molds, and traps gas in ways that no amount of post-processing can fully erase.
Cooling rate works more subtly. Fast cooling freezes a fine grain structure—more boundaries per unit volume, which generally means higher yield strength but often at the cost of ductility. Slow cooling lets larger grains grow, which can improve creep resistance in high-temperature service but weakens the material under sudden impact. The trick is that cooling rate is rarely uniform across a casting: a thin rib chills in seconds while an adjacent heavy boss takes minutes, creating a strength mismatch that can crack during service even if each region individually meets spec.
Foundries that understand this don't treat pouring and cooling as separate steps to be hurried through. They design gating systems to deliver metal at the right velocity for the section thickness, and they use chills, insulation, or mold materials to steer the cooling front deliberately. The result is a part whose strength profile matches its actual load path—not just a chemistry that looks good on paper but a microstructure that holds up where it matters.
Mold and Core Design Details That Lower Residual Stress
Residual stress in castings or moldings often starts with uneven heat removal. In mold and core design, placing cooling lines closer to thick sections and using baffles or bubblers inside deep cores evens out the temperature drop. When the entire part cools at a similar rate, the internal pulling forces stay low instead of concentrating near isolated hot spots.
Another detail that gets overlooked is how the metal or plastic enters the cavity. A gate placed to feed a thin wall before a thick boss can create pressure spikes that lock in stress. Shifting the gate or adding a small overflow well lets the material pack evenly, and designing cores with gentle transitions instead of abrupt steps helps the part shrink without fighting the tool.
Finally, the core itself can be made more forgiving. Adding a slight taper on ribs and bosses, or splitting a long core into two shorter inserts with a relief gap, reduces the mechanical grip that holds the part in a stressed state. These small changes in the tool geometry often do more to lower residual stress than adjusting process settings alone.
Late Inoculation Practices for a Finer, More Uniform Flake Structure
Adding inoculants late in the melt preparation, just before pouring, shifts the solidification dynamics in a way that early additions rarely achieve. Rather than letting nucleant particles drift or agglomerate during holding, late inoculation delivers a burst of active substrates directly into the cooling stream. The result is a marked reduction in flake size, but more importantly, the size distribution tightens. You no longer see the scattered coarse flakes that often form near thermal centers; instead, the structure settles into a consistent, fine pattern across the entire section.
This practice demands tighter process control, because the window between inoculation and solidification is short. Stirring, transfer time, and pouring temperature all influence how well the inoculant disperses before the matrix freezes. When timed correctly, though, late inoculation suppresses undercooling variability at the growth front, pinning graphite formation into a steady, repeatable rhythm. Foundries that adopt this approach often notice fewer hard spots and a more predictable response to machining, simply because the flake network no longer carries the same local irregularities.
Heat Treatment Cycles That Stabilize Dimensions Without Sacrificing Hardness
Dimensional drift in hardened components rarely stems from a single cause, but the usual culprit is retained austenite. When quenching leaves 10 to 20 percent austenite untransformed, that phase slowly decomposes at room temperature or during light service, swelling or shrinking the part by microns that matter in precision tooling. A stabilization cycle therefore begins by forcing that austenite to transform before final grinding or assembly. Multiple deep draws or a cryogenic soak immediately after quenching can convert most of the retained austenite to martensite, but the real trick is doing it without wrecking the freshly formed martensite. A short temper between the quench and the cold treatment lets the steel reorganize slightly, reducing the chance of microcracking when the remaining austenite pops into martensite.
The next step is a series of tempering cycles, not just one. Many shops default to a single two-hour temper at a comfortable temperature, then watch dimensions move after delivery. A better route uses three tempers with incremental temperature tweaks, allowing each cycle to settle the fresh martensite and convert any newly formed austenite. This doesn't mean raising the tempering temperature beyond the hardness target—rather, it means holding at the target temperature long enough for carbide precipitation to reach a stable plateau. The result is a hardness that stays within one or two Rockwell points of the as-quenched value, but with almost none of the stress that would otherwise release over weeks or months in the field.
For parts where even a few microns of movement cause problems, a final stress-relief step below the tempering temperature can be added. This low-temperature soak doesn't alter the martensite's hardness but allows dislocations to rearrange and residual stresses from machining or grinding to dissipate. The key is to sequence it after rough machining and before finish grinding, so the part sees no further thermal energy high enough to trigger structural change. When combined with a quench-and-temper schedule that keeps retained austenite below about 5 percent, these cycles yield parts that hold size for years without dropping into a softer range.
Non-Destructive Checks That Reveal Subsurface Defects Before They Spread
Surface inspections only tell half the story. Hidden cracks, voids, and delaminations often lurk beneath the outermost layer, developing quietly until they compromise structural integrity. Non-destructive testing (NDT) methods like ultrasonic pulse velocity, ground-penetrating radar, and infrared thermography let engineers peer into materials without causing further harm. By sending acoustic waves, electromagnetic signals, or thermal gradients through concrete, steel, or composites, these techniques map internal irregularities in real time. The result is an early warning system that pinpoints weak zones long before they become visible—or catastrophic.
Each method has its own sweet spot. Ultrasonic testing excels at gauging concrete density and locating deep fractures, while radar penetrates reinforced slabs to reveal rebar spacing and moisture pockets. Thermography, on the other hand, detects air gaps and delaminations by reading surface temperature variations after a controlled heat pulse. What makes these checks truly powerful is their repeatability: the same scan can be performed weeks or months later to track whether a micro-crack is stable or actively spreading. This longitudinal view turns a one-time assessment into a dynamic health record for the asset.
The real value lies in timing. A subsurface flaw caught during routine inspection costs a fraction of what emergency repairs demand after the defect breaks through. Facilities managers and bridge inspectors increasingly rely on these silent sentinels to prioritize maintenance budgets and extend service life. Rather than waiting for spalling, rust staining, or sudden settlement to sound the alarm, they let physics do the detective work—mapping the invisible, measuring the inaudible, and flagging risk while there's still room to act.
FAQ
The difference usually comes down to graphite shape and matrix control. A uniform distribution of type A flakes in a pearlitic matrix gives the best blend of strength, wear resistance, and machinability. Undercooled or interdendritic graphite, by contrast, tends to create microcracks and lower fatigue life.
Stay close to the eutectic point, usually around 3.9 to 4.1 for smaller sections and lower for heavy sections. This encourages good fluidity and reduces shrinkage while keeping the pearlite/ferrite balance workable. Too much carbon gives coarse flakes, and too little raises the risk of chill.
Inoculation controls how carbon solidifies rather than how much is present. A late addition of fine-grained ferrosilicon supplies extra nucleation sites, which promotes fine, evenly spread type A flakes and limits undercooling. That leads to better tensile strength and more uniform hardness across the casting.
Thick sections cool slowly and can develop coarse graphite plus a soft ferritic matrix if no adjustment is made. Thin sections can chill and form carbides. Balancing chemistry, inoculant amount, and using chills or insulation helps each section reach a similar, sound microstructure.
Small additions such as copper, tin, or molybdenum stabilize pearlite and refine the structure. Copper up to about 0.5% raises strength and hardness without promoting massive carbides, while molybdenum helps retain strength at elevated temperatures. The goal is a fully pearlitic matrix, not hard spots that ruin machinability.
Stable sand compaction, proper moisture control, and good venting reduce gas defects and rough surfaces that act as stress raisers. Consistent green sand properties give better dimensional accuracy and less heavy grinding, which can introduce residual stress. A clean surface also supports fatigue resistance.
Not always, but it pays off for parts that will see cyclic loads or precision machining. Heating to roughly 550–600°C and cooling slowly removes residual stresses from uneven cooling and handling. Skipping it on a highly stressed part can lead to distortion after machining or early cracking in service.
A non-pressurized gating system with the choke at the sprue base and generous runners keeps turbulence low. Place risers where they can feed the last areas to solidify, and use side risers or chills to create directional solidification. This reduces shrinkage porosity while avoiding reoxidation defects that weaken the part.
Conclusion
Gray iron's reputation for strength and durability rarely comes from meeting a generic chemistry card. The most reliable foundries adjust carbon, silicon, and manganese beyond minimum specifications, paying close attention to carbon equivalent and trace elements like sulfur and nitrogen to control graphite shape and matrix hardness. But even the best melt chemistry can be undone by careless pouring and cooling. Strength is largely set in the minutes after metal enters the mold: slower, controlled cooling through the eutectic range produces a more uniform pearlitic matrix, while rapid quenching can create hard, brittle carbides and locked-in stress. Mold and core design matters just as much. Using generous fillets, balanced section transitions, and collapsible cores lowers residual stress and reduces the risk of hot tears or distortion before the casting even reaches the shakeout table.
Late inoculation is one of the most underused tools for improving gray iron. Adding a small amount of inoculant just before or during pouring refines the flake graphite, yielding a finer Type A structure that improves machinability, tensile strength, and fatigue resistance. After casting, controlled heat treatment cycles—often a low-temperature stress relief or a subcritical anneal—can stabilize dimensions without softening the matrix beyond acceptable hardness, which is critical for precision components that will see thermal cycling in service. Finally, non-destructive checks such as ultrasonic testing, resonant frequency analysis, and dye penetrant inspection catch subsurface flaws like shrinkage, gas porosity, or microcracks long before they grow into field failures. Combining these practices—from melt adjustments and cooling control to late inoculation, targeted heat treatment, and rigorous inspection—builds gray iron castings that consistently deliver superior strength, dimensional stability, and long-term durability under demanding loads.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/