Best Lost Foam Casting Techniques for High Quality Metal Parts
2026-10-12
What separates a mediocre lost foam casting from a high-quality metal part? Often, it’s not the alloy or the equipment—it’s the technique. In this post, we look at the best lost foam casting methods that consistently deliver dimensional accuracy and surface finish, including practices refined by Zhaoyuqi. The next few minutes could change how you approach your next pour.
Foam Density Selection for Stable Patterns
Foam density matters more than most people realize when you're trying to keep a pattern from shifting or losing its shape. A foam that's too soft will collapse under repeated pressure, causing fine lines to blur or deep impressions to flatten out. On the other hand, going overly dense can make the foam feel rigid, which works against you when you need a slight give for even ink or paint transfer. The sweet spot usually sits somewhere in the middle, but it depends heavily on the level of detail your pattern demands.
For stable, repeatable results, start by matching the foam density to the smallest feature in your design. If your pattern includes tight corners or thin bridges, you'll want a higher-density foam—something that resists curling at the edges and won't sag into the gaps. A quick hand test can tell you a lot: press your thumb firmly into the foam and watch how fast it springs back. A slow recovery suggests it will hold a distorted shape over time, while a snappy rebound typically means it will keep your pattern crisp through multiple uses.
One trick that isn't talked about enough is to test the same pattern on two different densities before committing to a full run. Cut small blocks from a 25 kg/m³ foam and a 40 kg/m³ foam, apply your pattern with the same pressure, and compare the edge sharpness after ten impressions. You'll often find that the lower-density option works fine for broad, open shapes, but the higher density wins for fine-line work. This side-by-side check removes the guesswork and gives you a repeatable reference for future projects.
Refractory Coatings That Stop Metal Penetration
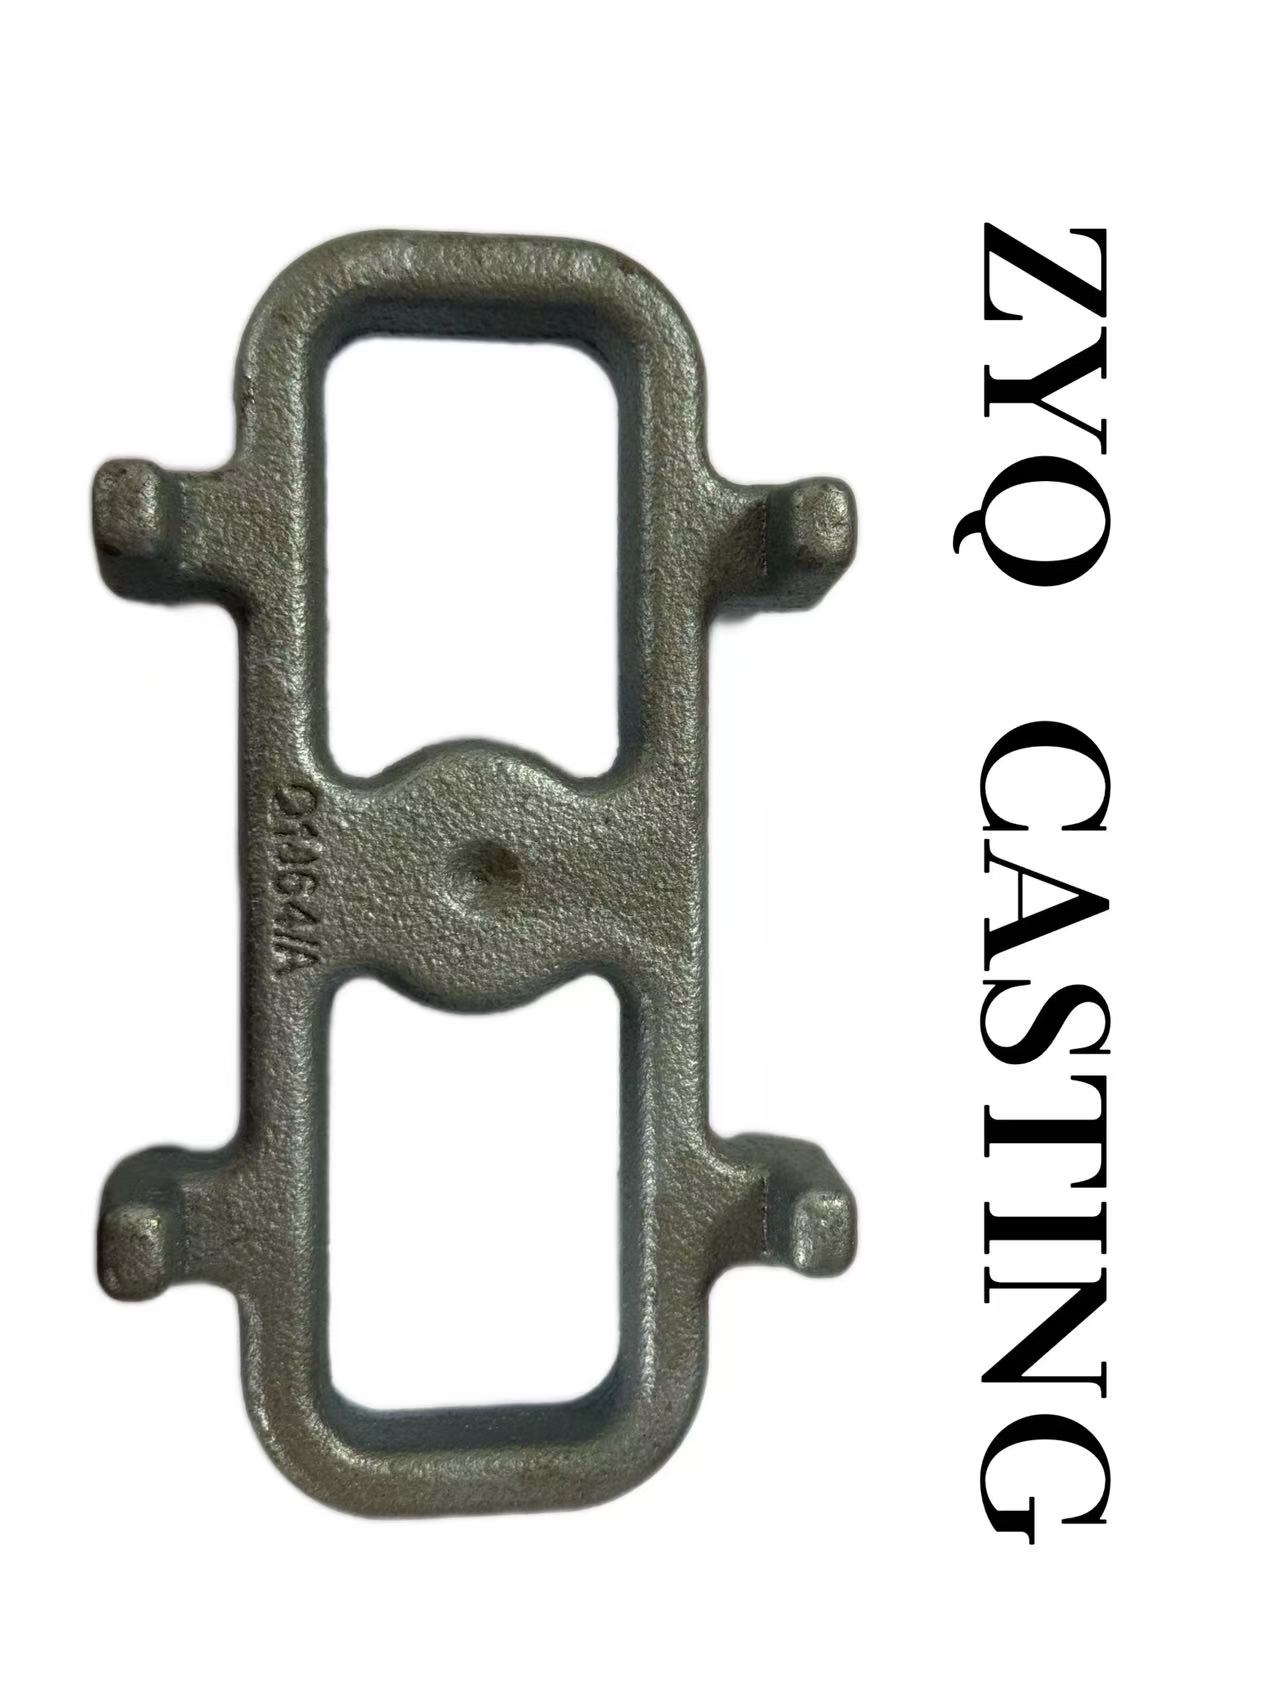
When molten iron or steel contacts a mold wall, it does not simply push against the surface. It seeks out every tiny void between sand grains and climbs into them through capillary action. A refractory coating stops that movement by presenting a dense, smooth, and chemically stable face to the metal. Good coatings are not just paint; they are the final line of defense between a clean casting and one covered in burn-on, veining, or penetration defects.
The coating's performance depends on its filler system and how those particles sinter under rapid heating. Zircon and alumina remain inert and do not wet easily, so the metal pulls back instead of soaking in. Some foundries add a low-melting frit that softens just before the metal arrives, forming a temporary glaze that bridges microcracks in the coating. That glaze then re-dissolves or stays as a harmless skin on the casting surface.
In practice, the best refractory coating fails if it is brushed on too thin at a deep pocket or sprayed unevenly in a narrow cavity. Experienced molders check for dry spots and build up extra layers in high-pressure areas like ingates and riser contacts. A consistent film, typically between 0.2 and 0.5 mm dry thickness, keeps the barrier intact and prevents localized metal intrusion without risking coating spall.
Gating and Riser Design for Even Filling
Getting metal into the mould without turbulence sounds simple until you watch a short shot. I have found that the most reliable way to promote even filling is to choke the runner before the ingates, using a well-radiused sprue base and a runner extension that traps the first cold metal. For tall castings, a stepped ingate arrangement works better than a single bottom gate because it keeps the rising metal front from folding over itself. The key is to keep the metal velocity under about 0.5 m/s at the ingate for most aluminium and copper alloys, and to make the total ingate area roughly equal to the runner area after the choke.
Riser placement then has to support the filling pattern rather than fight it. A riser that sits directly over a hot spot but too close to an ingate can draw metal away from the last area to fill, creating a cold shut or misrun. I usually offset the riser slightly downstream of the ingate entry or neck it down with a small contact so it stays liquid longer without stealing the flow. On plate-like sections, using a blind riser with an insulating sleeve and a breaker core helps maintain directional solidification while keeping the metal level in the cavity more uniform during the pour.
In practice, I always run a water analogue or a quick simulation before cutting steel, especially when the casting has thin ribs branching off a thicker wall. Even a small change in ingate angle from 30 to 45 degrees can shift the fill time enough to cause air entrapment at the far end. The goal is not just even filling, but an even temperature gradient across the filling front, so the riser sees hot metal last and begins feeding before the gate freezes.
Vibration Compaction for Thin-Walled Sections
Thin-walled sections pick up vibration energy unevenly. The form faces flex, the concrete can bridge over narrow gaps, and the wall ends up with shadow zones or honeycombing if the settings are left at what works for a massive column. A better starting point is to cut the amplitude and raise the frequency, then watch how the mix responds along the full height instead of relying on a single probe reading.
On site, that usually means attaching small external vibrators directly to the form at tight spacing and cycling them for short bursts rather than running one large internal poker down the middle. The lifts need to stay thin enough that air can travel to the surface before the next layer locks it in. Over-vibration is just as harmful here as under-vibration because it can push paste out of the wall and leave the aggregate skeleton loose. When the rhythm is right, the wall compacts from the form inward and the surfaces come out dense without bulging or form staining.
Pouring Temperature and Speed for Clean Castings
In metal casting, the temperature at which molten metal enters the mold dictates more than fluidity—it sets the stage for surface quality. Pour too hot, and the metal may erode sand molds or react with gases, trapping oxide films that end up as inclusions. Pour too cool, and the metal can begin to solidify before filling thin sections, leaving cold shuts or misruns. The sweet spot varies by alloy, but it’s often just above the liquidus temperature, where the metal remains fluid enough to replicate fine details without aggressive mold interaction.
Pouring speed works hand in hand with temperature. A slow, steady pour can allow gases to escape through the mold’s permeability, but drag on too long and the metal cools unevenly, promoting turbulence at the sprue base. A fast pour might fill the cavity quickly, yet it risks splashing and air entrainment, which create porosity and dross. Skilled foundry workers adjust the pour rate to match the gating design—narrower runners demand a more controlled stream, while larger castings may benefit from a slightly faster but still laminar flow.
For truly clean castings, the goal is to keep the metal front advancing smoothly and continuously. This often means pouring from a consistent height, using a well-designed basin to reduce velocity, and maintaining temperature within a narrow band. Small shifts in either variable can decide whether a casting comes out with a bright, defect-free skin or requires grinding and weld repair. Monitoring both temperature and speed at the pour station isn’t just process control—it’s the difference between scrap and a sellable part.
Cooling Curves That Prevent Distortion
The shape of a cooling curve often matters more than the final temperature. A rapid, uniform quench might sound efficient, but it can set up steep thermal gradients that leave residual stress locked inside a part. Distortion creeps in later, during machining or even in service, as those stresses slowly redistribute. Instead, a controlled cooling path with deliberate pauses at intermediate temperatures gives the material time to relax without triggering unwanted phase changes all at once.
For many alloys, the real trick lies in how you pass through the transformation range. Holding briefly just above martensite start, for example, lets hotter sections cool while colder sections catch up, reducing the mismatch that drives warping. In precipitation-hardening grades, a stepped cooling profile can avoid coarse precipitates and keep the whole cross-section responding more uniformly. The exact curve isn't universal—it shifts with section thickness, alloy chemistry, and whether you're dealing with a forging, weldment, or additively manufactured part.
Practical setups often combine furnace cooling, forced air, and controlled quenchants to trace a path that looks almost hesitant on a time-temperature plot. Instrumented trials with embedded thermocouples help refine that path: you look for the cooling rates that keep flatness within tolerance without sacrificing hardness or toughness. Over time, these curves become part of a shop's internal knowledge—small adjustments in the cooling recipe can make the difference between parts that need straightening and parts that go directly to final inspection.
FAQ
Around 1.2 to 1.5 pounds per cubic foot works well for most ferrous and aluminum alloys. Heavier foam leaves more carbon residue, while lighter foam can deform during sand compaction, so staying in that middle range usually gives a cleaner metal fill.
Use a thin, permeable refractory coat and make sure it dries fully before the flask is filled with sand. If the coat is too thick or has trapped moisture, the sudden heat makes it spall and the metal can push sand into the casting.
High frequency, low amplitude vibration packs sand into deep recesses without shifting the foam pattern. Heavy amplitude can bow thin sections or move internal cores, so adjusting the table to around 60 to 90 Hz often gives a more stable mold.
Pour at the low end of the alloy's temperature range and add a small riser directly over the heaviest section. The lower heat input gives the foam gas time to escape through the coating instead of getting trapped in the metal.
Yes, but you have to screen out the burned coating lumps and any unvaporized foam beads first. The sand also loses some of its binder over time, so adding a small percentage of fresh sand each cycle keeps the compaction consistent.
Lost foam lets you glue several foam sections together into a single pattern, so you can create undercuts and internal passages without needing cores. Green sand would require complex core prints and extra assembly, which adds cost and tolerance stack-up.
Apply the refractory coating in thin layers and let each one dry completely before the next. A stiff coating shell supports the pattern during sand fill, and storing patterns flat instead of hanging them also avoids warping from their own weight.
Conclusion
Choosing the right foam density sets the tone for everything else in lost foam casting. A denser bead structure resists distortion during handling and coating, but if it's too dense the metal has a harder time displacing it cleanly. Most shops settle on a middle range that holds pattern dimensions without leaving excessive carbon residue. Once the pattern is stable, the refractory coating becomes the real barrier against burn-on and penetration. A thin, even layer that dries without cracking allows the metal to flow smoothly while keeping sand from invading the surface. Gating and riser placement then decide whether that flow reaches every corner evenly. Keeping gates low and risers close to heavy sections prevents cold shuts and shrinks. For thin-walled parts, vibration compaction is often overlooked. Short bursts at moderate frequency pack sand into deep pockets without crushing the foam or shifting the pattern, which is far better than long, aggressive shaking.
Pouring temperature and speed matter more than many foundries admit. Pouring too hot erodes the coating and increases gas defects, while pouring too cold causes misruns in thin sections. A slightly lower superheat with a steady, uninterrupted pour usually gives the cleanest metal because the foam vaporizes ahead of the advancing front instead of being trapped. Cooling curves are the final piece. Letting the casting cool unevenly introduces residual stress that shows up as distortion after shakeout. Placing chills near heavy bosses or using insulating sleeves on thin walls evens out the thermal gradient. In practice, these techniques build on one another: a stable pattern with a sound coating, a well-placed gating system, careful compaction, and controlled pouring and cooling produce parts that need far less grinding and straightening.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/