Vertical Lift Rack Zinc Plating Equipment Company Qualities That Ensure Consistent Coating Performance
2026-11-16
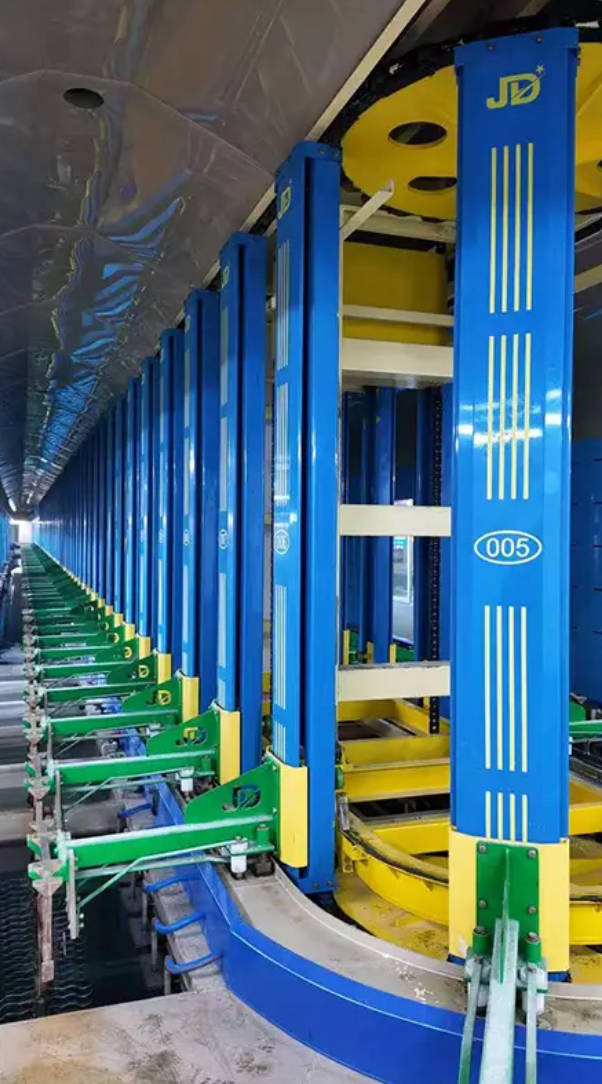
Coating consistency is rarely decided by the plating bath alone. On a vertical lift rack zinc line, the way parts are fixtured, immersed, and withdrawn has an outsized impact on thickness distribution, adhesion, and post-plate corrosion resistance. Unless the equipment is designed to control those variables cycle after cycle, even a well-run bath will produce unpredictable results. Junda builds vertical lift rack zinc plating systems around those overlooked mechanical details, not just tank dimensions. The qualities covered below are the ones that show up in coating performance long after the purchase order is signed.
Lift Mechanics That Hold the Same Withdrawal Curve
A withdrawal curve is the line the bar traces from the floor or rack position to full lockout. When that curve stays nearly identical from set to set, the movement becomes less about raw effort and more about repeatable mechanics. Small deviations early, like the bar looping forward around the knees or the chest dropping, force the body to reorganize under load. The lifts that hold the same curve tend to keep the bar close to the body, the shoulders slightly ahead of the bar until the hips extend, and the feet quiet on the floor.
Holding that curve under fatigue is what separates a clean session from a sloppy one. As the last reps get hard, the temptation is to yank the bar off the ground or to let the descent collapse. Instead, lifters can slow the first few inches, keep the same knee and hip timing, and let the bar come down along the route it went up. Those small technical anchors make the withdrawal curve stable even when the load feels heavy, which usually leads to more consistent speed and fewer missed lifts at the edge of a max.
Rectifier Response Tuned for Mixed Rack Loads
Rectifier response tuning doesn't get much attention until someone plugs a mix of blade servers, GPU boxes, and storage shelves into the same rack and wonders why the bus voltage starts to wander under step loads. The issue rarely comes from a single converter; it comes from how several rectifiers share the transient when all those different load characteristics hit at once. A purely resistive load lets a stock control loop look almost over-damped, while the same loop turns soft and lazy against capacitive storage shelves, then rings against high di/dt server draws. Tuning for a mixed rack means accepting that the aggregate load is neither constant-current nor constant-power in any useful sense, so the rectifier's crossover and recovery behavior have to be set with headroom for the worst combination rather than the average.
One practical approach is to treat the rack as a composite impedance rather than trying to model each device separately. The rectifier's voltage loop can be skewed slightly faster than the slowest bulk capacitor bank would normally prefer, while the current limit response stays conservative enough to avoid slew-rate fighting between parallel units. In a mixed rack, the trick is to keep the rectifier from overcorrecting when storage shelves demand a slow recharge after a GPU burst, yet still hold the bus tight enough that blade servers don't trip undervoltage monitors. That middle ground usually comes from raising the phase margin a few degrees beyond what a purely resistive bench test suggests and reducing the integrator windup during short overloads.
Field adjustments rarely follow a fixed formula because the ratio of capacitive, inductive, and switching loads changes from rack to rack. A useful habit is to probe the DC bus under a scripted load sequence that alternates between idle, storage recharge, and full server compute, then nudge the rectifier response until the bus settles without a visible second dip or a long tail. If the recovery looks clean on the storage-only step but collapses when servers are added, the loop is being fooled by the load's negative resistance at certain operating points. Tweaking the rectifier's feedforward term and limiting its rate of change often restores a neutral response without the oscillatory signature that stock tune files tend to leave behind.
Agitation That Reaches the Low-Current Corners
Uneven metal deposition rarely announces itself across the open face of a part. It hides where the solution moves slowly: inside threaded holes, along sharp internal corners, beneath overhangs, and at the far edge of a rack where current density falls away. Simple air lines or a central mixer often leave these low-current pockets largely untouched, because the bulk flow follows the easiest path and skips the geometry that actually needs it. The result is a pattern of thin, dull, or slightly rough plating exactly where the part can least afford it.
The value of agitation designed for these zones is not just turbulence; it is delivery into the corners that might otherwise consume additive unevenly or trap a faint gas bubble. A well-placed eductor, a reciprocating paddle with a short stroke, or a directed flow bar across the back of the rack can push fresh electrolyte into those recesses. When that happens, the local depletion layer thins out and the low-current areas begin to respond. The effect is often easier to see in the plating window than in the flow meter: burn-free edges, brighter recessed areas, and a thickness spread that no longer widens with each cycle.
It also helps to treat agitation as a positioning problem rather than a power problem. More pumping does not automatically reach a shielded corner if the nozzle orientation simply reinforces an existing circulation loop. Small changes—aiming the flow across the part rather than at it, alternating pulse sequences, or adjusting the paddle to sweep close to the cathode—can move fresh solution into areas that were previously stagnant. In low-current corners, that kind of deliberate agitation often does more for deposit quality than raising the average current density ever will.
Thermal Stability Across a Full Shift
Long shifts rarely expose a material's true thermal behavior in the first hour. The more revealing pattern appears later, once heat has soaked through housings, seals, and contact points. Across eight or ten hours of continuous operation, tiny changes in ambient temperature, load, and airflow begin to stack, and a component that looked stable at midday can drift by late afternoon.
What matters most is not the peak temperature reading but how tightly that reading holds over time. A well-designed system may show a slight upward curve during the first third of the shift, then flatten out as thermal expansion settles and contact resistance stabilizes. If the curve keeps climbing, or if it oscillates with each duty cycle, the issue is rarely the sensor—it is usually heat being trapped where it should not be.
Field checks tend to focus on start-up and end-of-shift values, but the middle hours often hide the real story. Seasonal drift, dust buildup on cooling surfaces, or a worn thermal interface can all produce a slow, steady rise that only becomes obvious when data is plotted across the full shift rather than sampled at convenient intervals.
Contact Points Checked Before Resistance Drifts
Before chasing a drifting resistance reading, the first thing worth checking is whether the measurement contacts are actually stable. A slightly oxidized pad, a probe that has lost its spring tension, or a connector that is not fully seated can easily produce changes that look like drift in the material itself. Cleaning the contact area and reseating the test leads often removes the apparent instability without any further adjustment to the setup.
It also helps to repeat the measurement several times after moving the probes or reconnecting the fixture. If the readings shift with each reconnection but settle when the contacts are held firmly, the drift is more likely mechanical than electrical. In those cases, checking the contact points before adjusting the measurement range or looking for temperature effects saves time and prevents chasing false failures.
Post-Run Measurements That Shape the Next Run
The data collected after a run often gets treated as a scoreboard, but the most useful way to look at it is as a tuning note for the next session. Rather than simply checking whether you hit a pace target, pay attention to how your heart rate drifted during the final third of the distance, how long it took for your breathing to settle, and whether your cadence stayed even when fatigue set in. Those small shifts tell you more about readiness than a single average number ever will.
A common habit is to run the same route and chase the same finish time, but post-run measurements can point you toward a smarter variation. If your stride length dropped noticeably in the last two kilometers while cadence stayed high, the next run might benefit from a shorter distance with a few relaxed strides instead of another long effort. If your resting heart rate the morning after was still elevated, that is a quiet signal to spend a day on recovery rather than pushing through another hard session.
There is also a tendency to overreact to a single bad run. One sluggish split or a slightly higher average heart rate does not mean your fitness has collapsed. Compare a few runs under similar conditions before making changes. The real value of measuring what happens after you stop running is not in judging the past workout but in deciding how much load, speed, or rest your body actually needs tomorrow.
FAQ
The difference usually comes down to how well the builder manages current flow, bath movement, and part orientation at the same time. A dependable line uses rigid rack frames, maintained contact points, balanced anode placement, and controlled lift timing so each section of the part sees similar plating conditions.
Rack design sets the path for current and the distance between the part, anodes, and tank walls. Well-placed contacts reduce resistance hotspots, while spacing that avoids shielding lets the bath reach recessed areas. That helps deposit zinc evenly instead of building up on edges and leaving low spots in the middle.
Lift speed changes how quickly the part enters and leaves the bath, which affects drainage, rinsing, and the transition time before plating current stabilizes. Consistent dwell keeps every load in the solution for the same interval, so thickness per cycle stays repeatable rather than drifting from rack to rack.
Rectifier ripple, busbar layout, contact resistance, and current ramping all matter. A thoughtful builder sizes conductors to avoid voltage drop at the far end of the line, uses clean contact points, and sets rectifier controls that hold current density within a narrow band across the full load.
Tank geometry controls the distance between anodes and the work. Paired with agitation or solution circulation, it prevents temperature and concentration layers from forming. That kind of movement replenishes zinc ions near recessed surfaces, so deposition stays balanced instead of becoming edge-heavy.
A credible provider tests the frame alignment, lift travel, rectifier output, contact continuity, and tank circulation under load. They may run a dummy rack or sample parts to verify current distribution and timing, then document the results so the line arrives ready for process qualification.
Frames and contacts need to resist attack from cleaning acids and plating chemistry while maintaining conductivity. If contacts wear or coating builds up on the rack, resistance changes across cycles. Durable materials and a regular stripping schedule keep current delivery stable, which keeps thickness repeatable over months.
Look for a builder that provides clear setup parameters, troubleshooting guidance for thickness variation, and spare contact or anode recommendations. Teams that can adjust rectifier settings, check rack contact wear, and schedule preventive maintenance tend to hold a much tighter coating range.
Conclusion
Consistent coating performance on a vertical lift rack zinc line rarely comes from a single breakthrough. It emerges from lift mechanics that repeat the same withdrawal curve cycle after cycle, so parts leave the bath at the same speed and drain pattern every time. If the hoist hesitates or drifts, the zinc thickness shifts in hard-to-see areas. Rectifier response has to support mixed rack loads as well, since dense racks and open areas draw current differently. A power supply that reacts quickly but without spiking keeps current density more uniform. Agitation is equally important in low-current corners, where solution depletion causes dull or thin spots; flow has to reach these pockets rather than simply churning the center of the tank.
Thermal stability across a full shift matters because bath temperature changes viscosity, plating efficiency, and brightener behavior. Stable temperature removes one more variable from the process. Contact points are checked before resistance drifts, since worn or loose contacts can introduce local voltage drop that quietly ruins deposit uniformity. After each run, post-run measurements shape the next run: thickness readings, visual results, and distribution data guide adjustments to racking, current settings, or agitation. These measurements turn variation into a feedback loop instead of a recurring defect. Together, those qualities keep a vertical lift rack line predictable without forcing operators to rely on constant manual correction.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613575807672
Website: https://www.jundaelectroplating.com